Heat Exchangers
High-Performance Heat Exchangers for Industrial Applications
Metinox manufactures custom-engineered heat exchangers designed to deliver efficient thermal transfer, operational reliability, and long-term performance in demanding industrial environments.
Our solutions are built according to customer specifications and engineered to meet the highest standards of quality, safety, and efficiency.
References: Steam Boilers, Hot Water Vessels, Coil Heat Exchangers, Thermal Oxidizers
Our Heat Exchanger Solutions
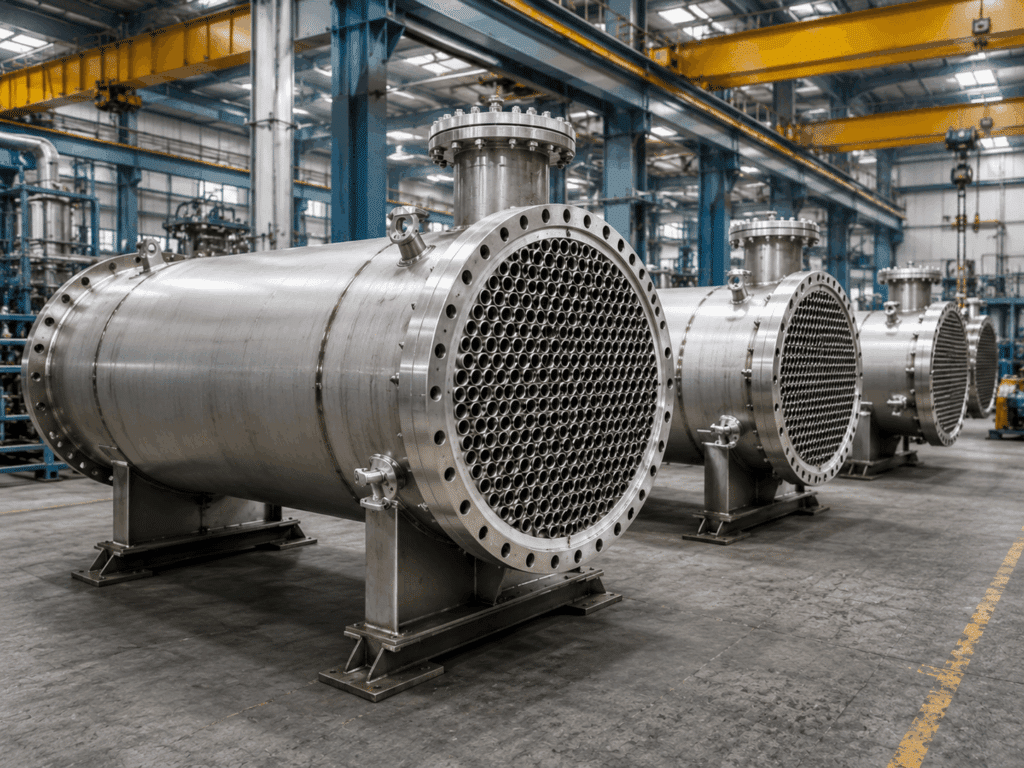
Shell & Tube Heat Exchangers
Custom-manufactured shell and tube units designed for high-pressure and high-temperature industrial processes.
Condensers
Efficient condensation systems engineered for industrial cooling and vapor processing applications.
Evaporators
Reliable thermal systems designed for controlled evaporation processes and industrial heat transfer operations.
Coolers
Industrial cooling equipment developed to maintain operational efficiency and temperature stability.
Economizers
Energy-efficient heat recovery systems engineered to optimize industrial process performance.
Custom Heat Transfer Equipment
Fully customized heat exchanger solutions manufactured according to client specifications and technical requirements.
Designed for Demanding Operating Conditions
Our heat exchangers are engineered to operate efficiently in complex industrial environments involving:
- High pressure
- Elevated temperatures
- Corrosive media
- Continuous industrial operation
- Critical process systems
We work closely with our clients to ensure each unit is optimized for thermal efficiency, mechanical reliability, and long operational life.
Advanced Materials for Maximum Durability
Metinox manufactures heat exchangers using a wide range of industrial-grade materials, including:
- Carbon Steel
- Stainless Steel
- Duplex Stainless Steel
- Super Duplex Stainless Steel
- Cu-Ni Alloys
- Clad Materials
Material selection is carefully adapted to operating temperatures, pressure requirements, corrosion resistance, and process compatibility.
Quality Control & Testing
All heat exchangers undergo comprehensive inspection and testing procedures throughout production to ensure safety, reliability, and performance.
Quality procedures include:
- Dimensional inspections
- Welding inspections
- Non-destructive testing (NDT)
- Hydrostatic testing
- Leak testing
- Material traceability verification
- Final quality inspections
Our commitment to quality ensures dependable equipment performance in critical industrial applications.